 contact@nxhdmfg.com
 +86 352 5330772
 +86 180 3528 0246
Structural steelwork is one of the few places where a bolt is not simply a bolt. Two assemblies arrive on site looking identical — same M20, same 10.9 marking, same galvanized finish, same box — and only one of them is permitted in the joint you have detailed. The difference is not the bolt. It is the standard the assembly was tested against, and what that test actually guarantees about the torque you will apply on site.
This guide explains what EN 14399 and EN 15048 each cover, why a preloaded joint needs a different product from a bearing joint, what "assembly" means in a certification sense, and what to put on an RFQ so that the material delivered matches the execution class on the drawing.
What the two standards actually cover
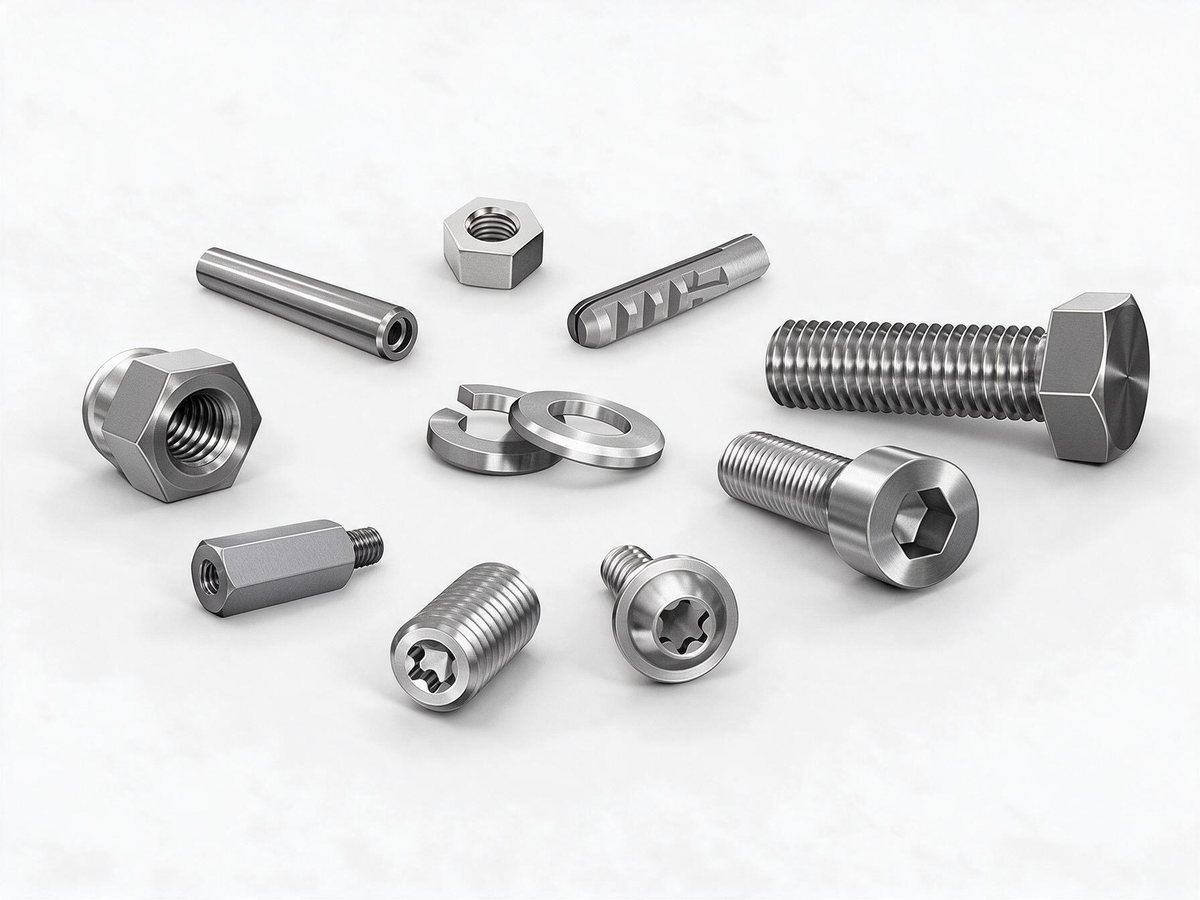
EN 14399 is the European standard for high-strength structural bolting assemblies for preloading. It runs to ten parts and defines three systems — HR, HV and HRC — built around hexagon bolt and nut assemblies in property classes 8.8 and 10.9, with nuts in classes 8 and 10.
The defining requirement is not tensile strength. It is consistency. An EN 14399 assembly is qualified by a suitability test (EN 14399-2) that demonstrates the torque coefficient of the lot stays inside a declared band, typically between 0.10 and 0.16 depending on the system and coating. A torque wrench set to one value has to develop a predictable clamp load in every bolt on the site, so scatter matters as much as the mean. A bolt that is strong but inconsistent fails the standard.
EN 15048 is the parallel standard for non-preloaded structural bolting assemblies. It has two parts and permits bolts in classes 4.6, 5.6, 8.8 and 10.9 with nuts in classes 5, 6, 8 and 10. It specifies dimensions, mechanical properties and marking, but it does not certify a torque-tension relationship, because the design does not rely on one.
Both products are legitimately "structural". The distinction is how the joint is expected to carry load, and that is a design decision rather than a purchasing preference.
Preloaded versus non-preloaded: what the joint is doing
A preloaded connection transfers load through friction between the faying surfaces. The bolt is tightened until the clamp force exceeds the service load, the plates do not slip, and the bolt itself sees very little shear. This is the logic behind slip-resistant connections in bridges, crane rails, moment frames and anything subjected to fatigue or reversals. Clamp load is everything, and clamp load is only predictable if the torque coefficient is controlled — which is precisely what EN 14399 certifies.
A non-preloaded connection transfers load by bearing: the plates bear against the shank and the bolt carries shear. Tightening is there to keep the joint closed and prevent loosening, not to generate a design clamp force. EN 15048 is built for this case. It is a simpler and less expensive product, and for a large share of ordinary steelwork it is entirely correct.
EN 1090-2 ties the choice to execution class and joint category. Slip-resistant connections at the higher execution classes call for preloaded assemblies to EN 14399, while bearing-type connections may use EN 15048. Where the project specification is silent, the safe move is to ask the engineer which joint category applies rather than to substitute upward or downward on your own authority.
Why the assembly is certified as a unit
This is where most procurement mistakes happen. The word "assembly" is not decoration. EN 14399 qualifies a bolt, nut and washer together, as a matched set, from a single manufacturer and a single lot. The suitability test is run on that combination.
Substitute a nut from a different supplier — even a nut that is dimensionally identical and marked class 10 — and the tested torque coefficient no longer describes what you are installing. The bolt may still reach the required preload, or it may not, and nobody will know until a tension check or a failure. The same applies to mixing bolts from two production lots within one connection, and to omitting the washer that the tested assembly included. Washers under EN 14399-5 and EN 14399-6 are part of the assembly, not an accessory.
For buyers, this has a practical consequence: structural bolting should be ordered as a complete assembly with a stated part number, and delivered and stored as a set. Splitting the order across suppliers to save a few percent on nuts defeats the certification you paid for.
Coatings, friction surfaces and the parts that are not in the standard
Hot-dip galvanizing to EN ISO 10684 is the usual protection for exposed structural bolting, and it changes the torque coefficient — which is why EN 14399 systems are declared with their coating in view. A galvanized assembly and a plain one are not interchangeable at the same wrench setting. If the design depends on a specific slip factor for the faying surfaces, that factor comes from the surface treatment of the plates, not from the bolt, and it is verified separately under EN 1090-2.
Where torque control is impractical — large diameters, restricted access, or a need to verify every fastener individually — the alternatives sit inside the same family: HRC assemblies with a calibrated preload (EN 14399-7 and -10), or direct tension indicators under EN 14399-9. These trade cost for verifiability.
It is also worth separating what the standard does not cover. Special-shaped parts, non-standard lengths, bespoke washer plates, bent or welded brackets and machined cleats fall outside the assembly standards entirely; they are non-standard parts and need their own drawing, material specification and inspection plan. A common source of confusion on fabricated packages is a mix of certified standard fasteners and uncertified special parts travelling in the same box, with a single certificate assumed to cover both.
What to put on the RFQ
A structural bolting enquiry that will produce usable quotations needs six things: the standard and part number down to the system and part (for example EN 14399-4, system HV); size and length in the standard format; property class for bolt and nut; the coating specification with its own standard reference; the certificate type required, usually EN 10204 3.1; and the execution class or project specification the material has to satisfy. Add marking requirements and any project-specific sampling instruction.
On delivery, check that the marking on the bolt head and nut face matches the certificate, that the system letter is present, and that bolt, nut and washer carry the same lot identification. Then confirm the certificate actually describes the assembly — a 3.1 certificate for bolts alone does not close the loop on a preloaded joint.
Conclusion
The choice between EN 14399 and EN 15048 is a question about the joint, not about the bolt. If the design relies on clamp load and friction, you need a preloaded assembly whose torque coefficient has been tested and declared, supplied as a matched set. If the design relies on bearing, a non-preloaded assembly is the correct and more economical answer. Getting this one line right on the RFQ prevents the most expensive kind of error in steelwork: material that is dimensionally correct, mechanically sound, and still not what the connection was designed around. Readers working through the mechanical side of the same decision may find our notes on bolt strength grade markings and preload force calculation a useful next step, and the certificate requirements are set out in more detail in our article on EN 10204 3.1 material certificates.
Key takeaways
- EN 14399 covers preloaded high-strength structural bolting assemblies in systems HR, HV and HRC, and certifies a torque coefficient band through a suitability test; EN 15048 covers non-preloaded assemblies and makes no such claim.
- The choice follows the joint: friction-grip and slip-resistant connections need preloaded assemblies, bearing connections do not.
- The bolt, nut and washer are qualified together. Substituting a component from another supplier or lot invalidates the tested behaviour.
- Coating is part of the assembly definition. Galvanized and plain assemblies are not interchangeable at the same torque setting.
- Special-shaped and non-standard parts sit outside these standards and need their own drawing, material and inspection specification.
Frequently asked questions
What is the difference between EN 14399 and EN 15048?
EN 14399 is the standard for preloaded high-strength structural bolting assemblies and certifies that the assembly develops a predictable clamp load at a given torque. EN 15048 covers non-preloaded structural assemblies, where the joint carries load in bearing and no torque-tension guarantee is made.
Can I use EN 15048 bolts in a preloaded connection?
No. An EN 15048 assembly has not been suitability-tested for torque coefficient, so the clamp load produced at a specified torque is not predictable within the band a preloaded design assumes. Use an EN 14399 assembly matched to the connection's execution class.
Can I replace the nut in an EN 14399 assembly with a class 10 nut from another supplier?
Generally no. EN 14399 qualifies the bolt, nut and washer as a tested set, and the declared torque coefficient applies to that combination. A dimensionally identical nut from a different source can change friction and alter the resulting preload.
Which standards and grades apply to structural bolting?
Structural bolting in Europe is governed by EN 14399 for preloaded assemblies and EN 15048 for non-preloaded ones, applied through EN 1090-2 execution classes. Bolts are typically property class 8.8 or 10.9, with nuts in class 8 or 10; coatings such as hot-dip galvanizing follow EN ISO 10684.
Does a structural bolt require a 3.1 certificate?
Most project specifications and CE marking obligations for structural fasteners call for EN 10204 type 3.1 inspection certificates, issued against the actual cast or lot. The certificate should cover the complete assembly, not the bolt alone, and its lot numbers must match the marking on the delivered components.
Does NXHD Manufacturing supply structural bolting assemblies?
NXHD Manufacturing produces standard fasteners, special-shaped parts and custom machined components at its Handan and Datong bases, and supplies OEM customers with assemblies and documentation packages matched to the drawing and the specified standard. Enquiries can be sent to contact@nxhdmfg.com with the standard, size, class, coating and certificate requirement.
Standards are revised periodically; confirm dimensions, grades and test requirements against the current edition of the standard and the project specification before release to production.
NXHD Manufacturing (contact@nxhdmfg.com) is a precision fastener and custom metal parts manufacturer with dual production bases in Handan and Datong, China. We supply standard and non-standard fasteners to OEM customers across Europe, the Americas and Asia.